Stop Heating the Air: The Real Way to Handle Powder Coating
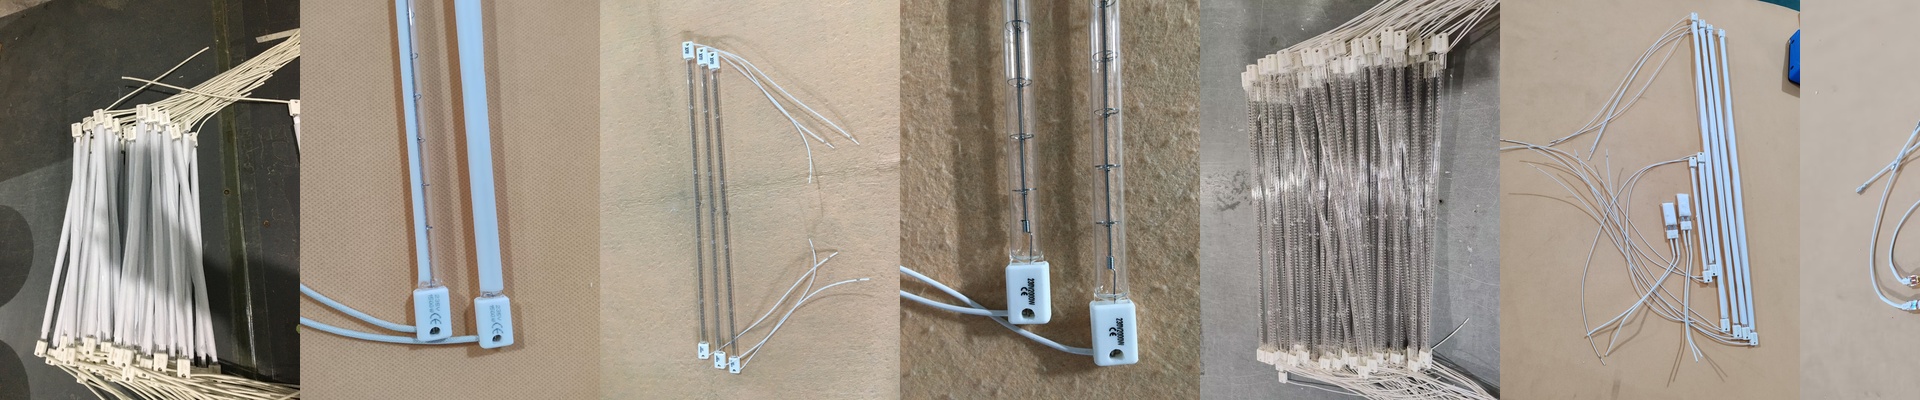
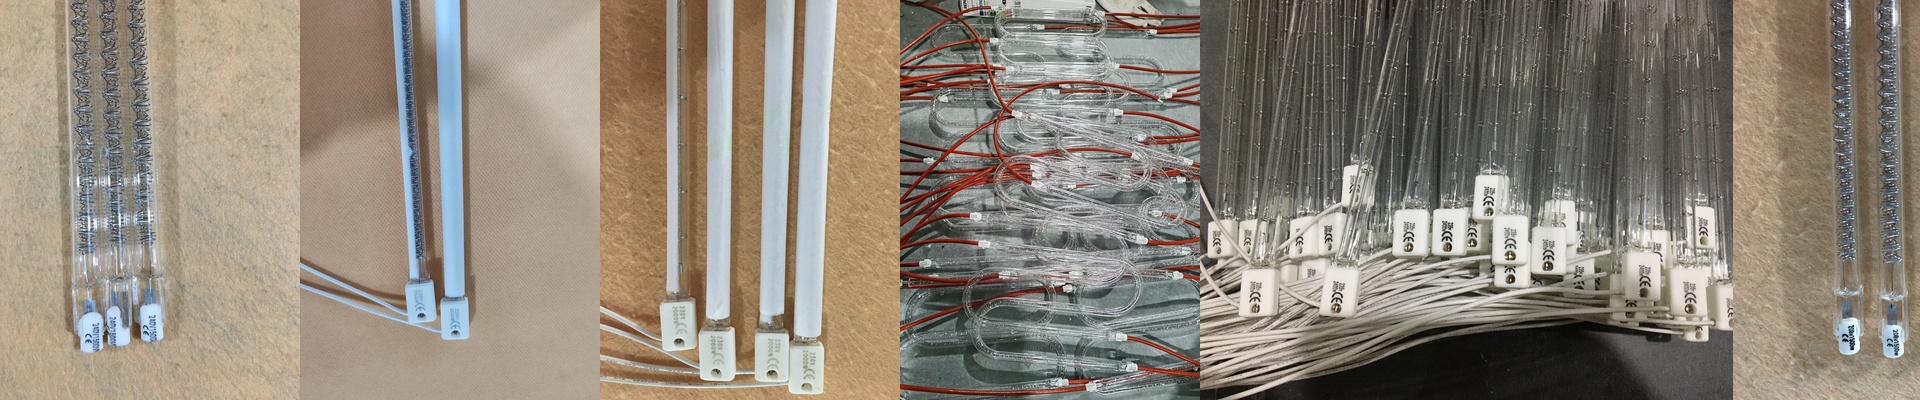
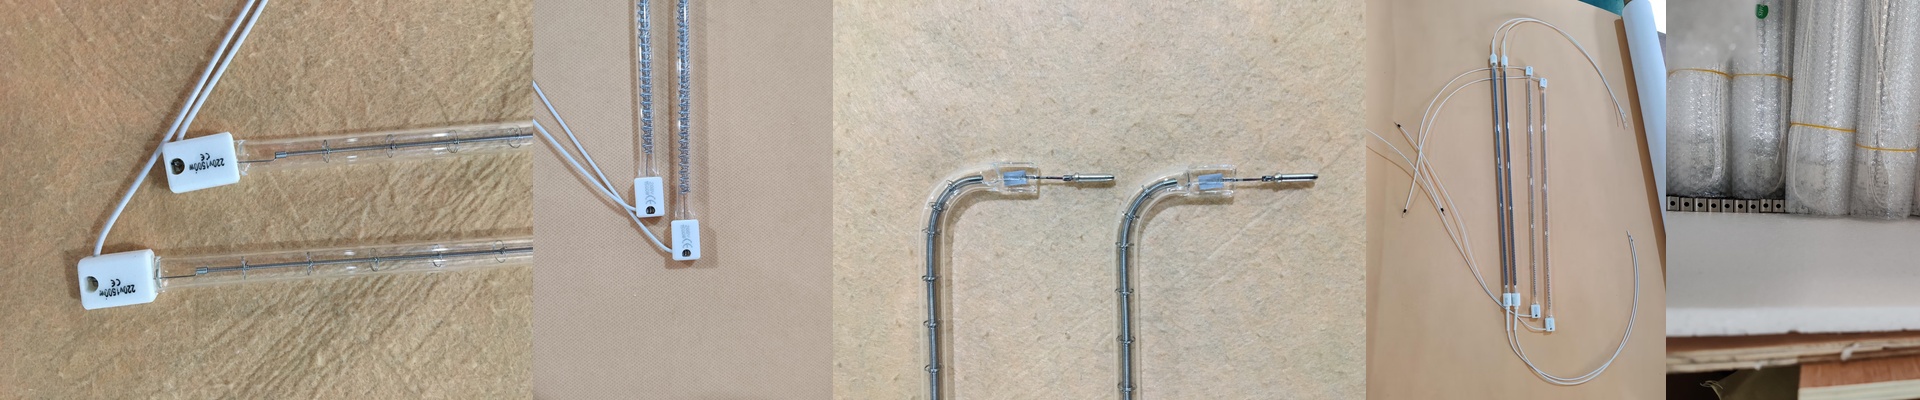
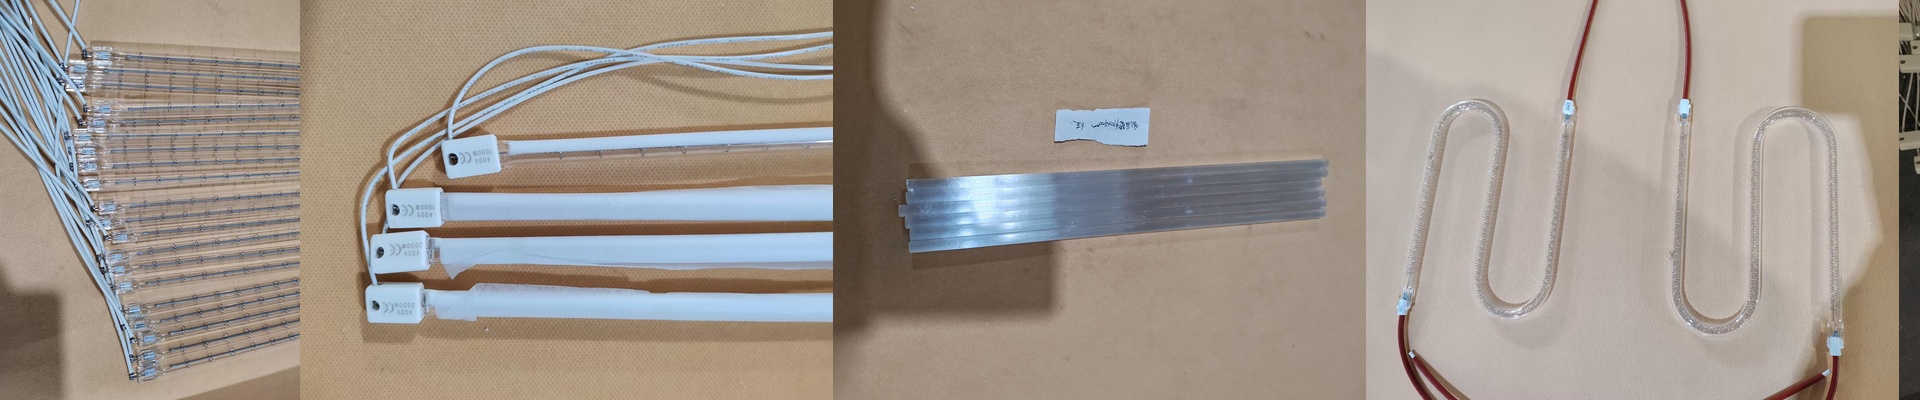
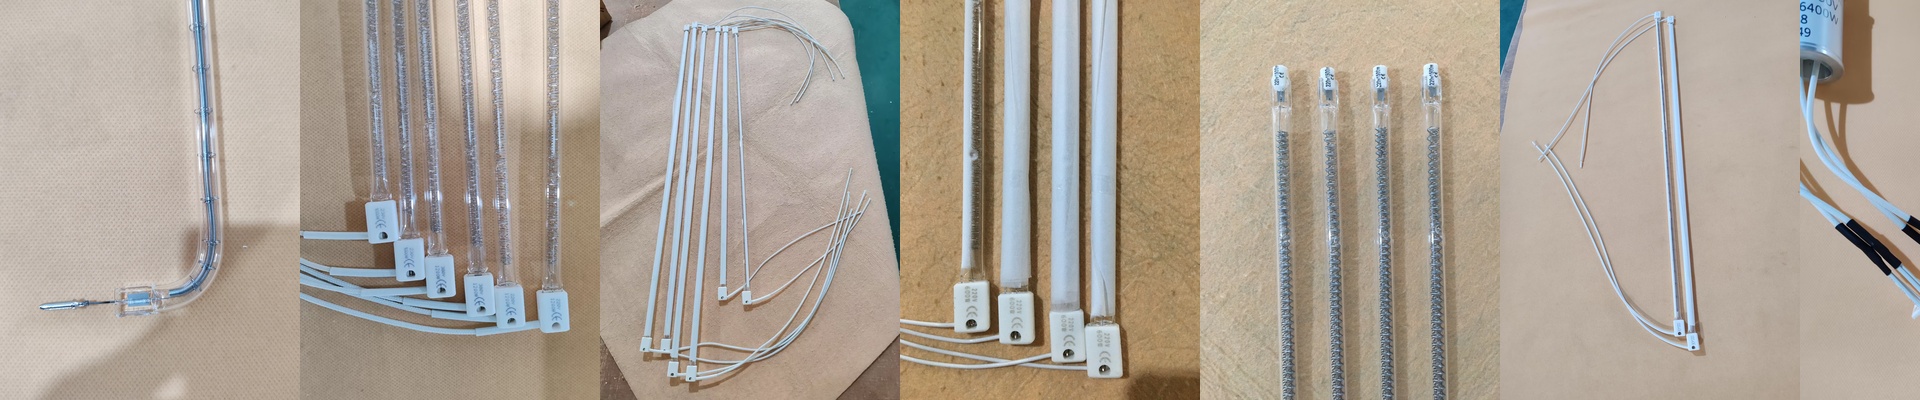
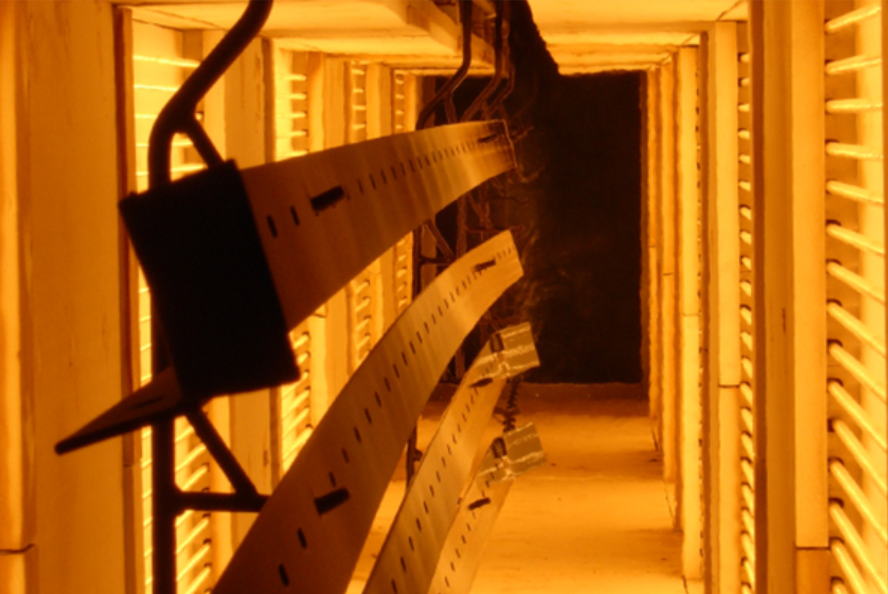
If you’re working in a low-margin business, every cent counts. And honestly? Spending money to heat up a giant room of air just to cure a few parts is a total waste. That’s why we use infrared (IR) curing lamps. Instead of waiting for the air to get hot, these lamps shoot energy straight into the powder. We stick with short-wave IR because it cuts right through the coating. It kicks off the cross-linking process in minutes. Not hours. Minutes. Getting the heat where it belongs To get things moving fast, you need a lot of power packed into a small space. We build our lamps to deliver a concentrated blast of heat. Why does that matter? Because it kills the “soak time.” You aren’t sitting around waiting for the metal to warm up. When you can drop your curing time from 20 minutes down to five, your whole day changes. You’re pushing more parts through the line without having to build a bigger factory. You just get more done per shift. Simple as that. The gear inside We use high-purity quartz glass for the tubes. If you don’t, the lamps will just crack the second they hit a rapid temperature swing. Inside, we use halogen-filled tubes. This keeps the filament stable so it doesn’t sag or burn out after a few weeks of hard use. If you’ve already got an array set up, these usually drop right in—just double-check that your controllers can handle the voltage and amp draw. The catch (and how to fix it) Now, here’s the thing. These high-density lamps put out a massive amount of heat. If you cram a high-wattage bank into a tight box without a plan, you’re going to melt your wiring and fry your sensors. You have to get your cooling fans and shielding right. Otherwise, your housings will warp, and you’ll be spending your weekend fixing equipment instead of shipping orders. At the end of the day, this isn’t about some fancy new trend. It’s about your electric bill. If your energy costs are eating your profits, stop paying to heat the air. Heat the part instead.